This page describes how to integrate and set up communication between OTC Welbee power sources and SmoothTool X.
Hardware Configuration
SmoothTool X is compatible with the robotic product series of the OTC brand. To set up communication between the software and a power source, the following items are required:
- One of the compatible OTC power source models:
- WB-P402L, WB-P502L
- If in doubt, contact your local OTC supplier or the Smooth Robotics team.
- Ethernet RJ45 cable from the power source to the robot.
IP Address
Select a valid IP address for the interface. The IP address must be on the same subnet as the robot. Configure it via the power source’s network settings.
Software Configuration
Once the hardware is configured, add and connect the OTC Welbee in SmoothTool X.
Add the OTC Welbee
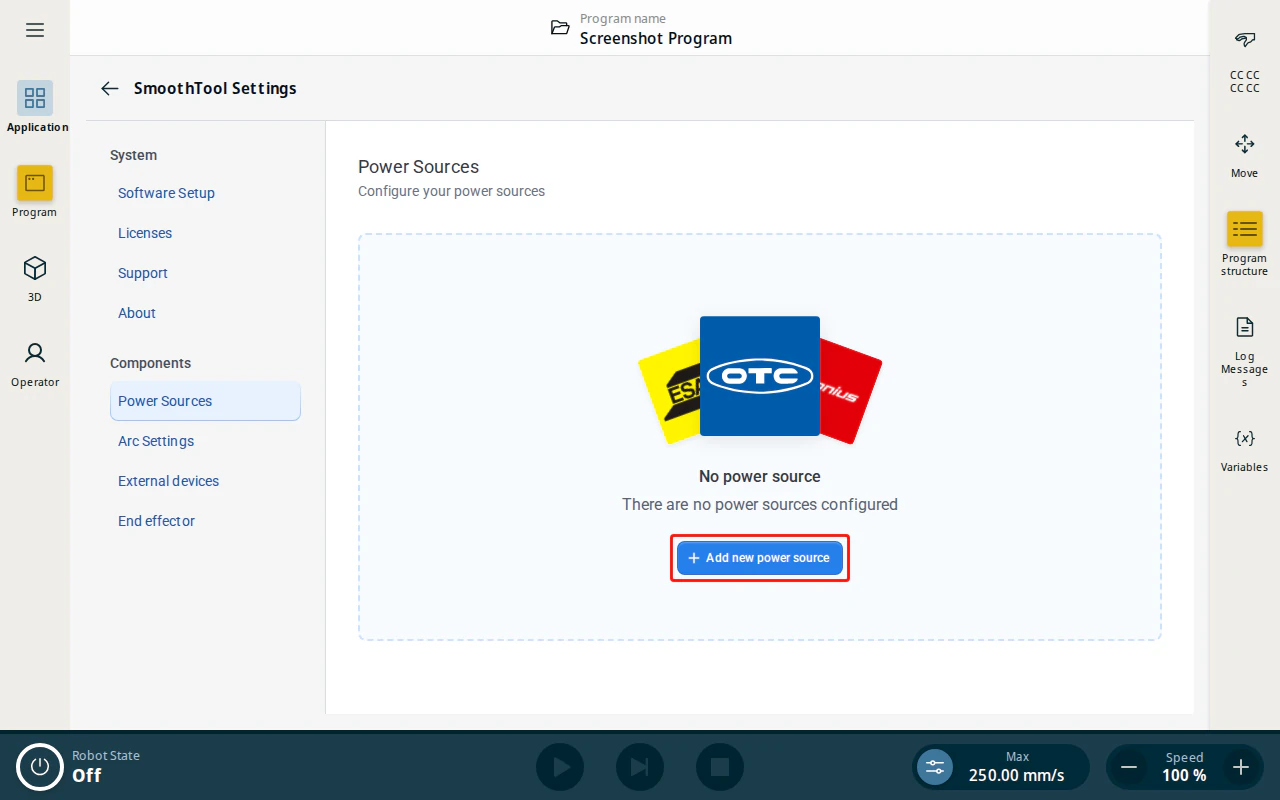
Tap SmoothTool X Settings from the Application view. In the sidebar, under Components, tap Power Sources, then tap Add new power source.
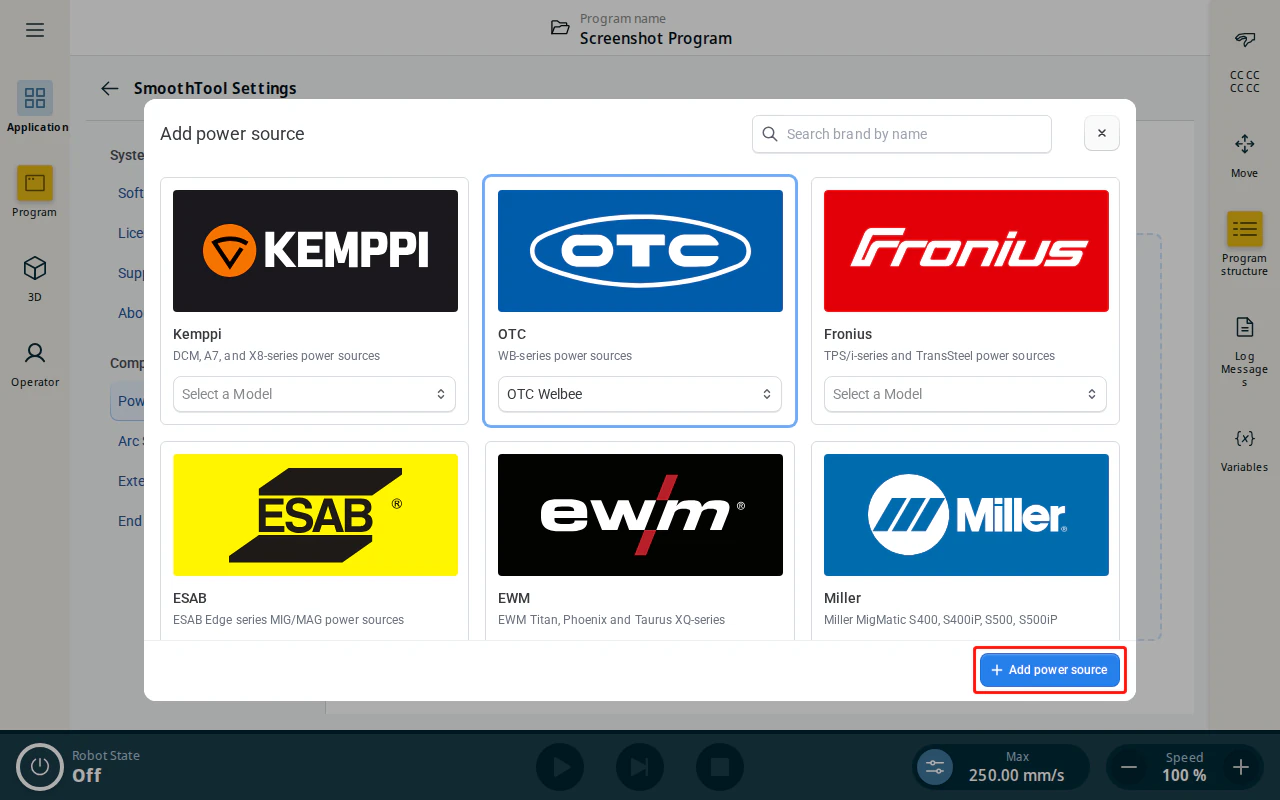
In the Add power source dialog, select the OTC tile and choose the OTC Welbee model, then tap Add power source.
Configure the OTC Welbee
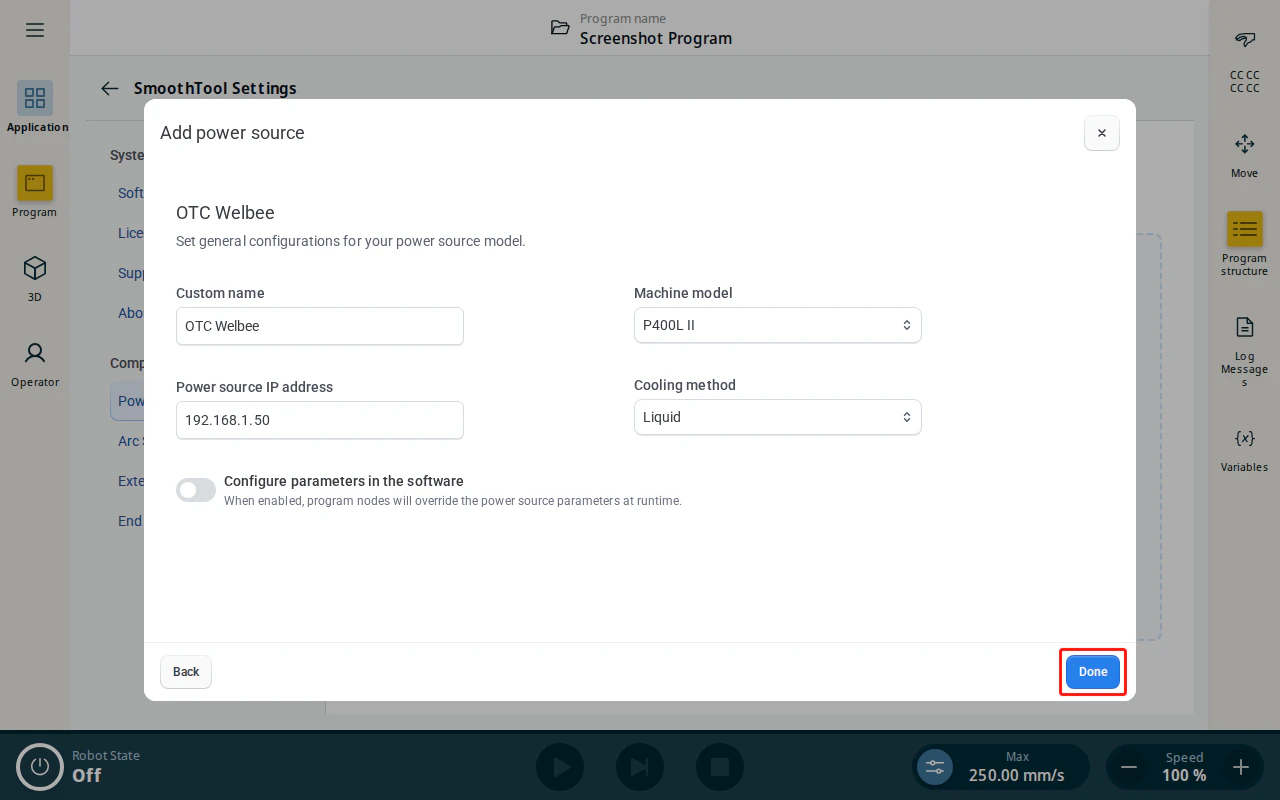
Fill in the configuration fields:
| Field | Description |
|---|---|
| Custom name | A name to identify this power source. |
| Power source IP address | The IP address of the power source. The robot uses this address to communicate with it. Ensure it is set correctly; otherwise the robot cannot connect. |
| Machine model | Select the machine model that matches your power source — P400L II or P500L II. This determines the available synergic lines. |
| Cooling method | Whether the torch is liquid– or gas-cooled. |
| Configure parameters in the software | Controls whether program nodes override the power source parameters at runtime — see Configure parameters in the software below. |
Caution
Select the correct Machine model for your setup. If the wrong model is selected, activation and connection will not be possible.
When done, tap Done to save the power source.
Configure parameters in the software
The Configure parameters in the software toggle controls how welding parameters are applied:
- Disabled (default) — the power source keeps the parameters set on the machine; program nodes do not override them.
- Enabled — program nodes override the power source parameters at runtime, letting you set welding parameters per node from the Power Source Parameters node.
Connect to the OTC Welbee
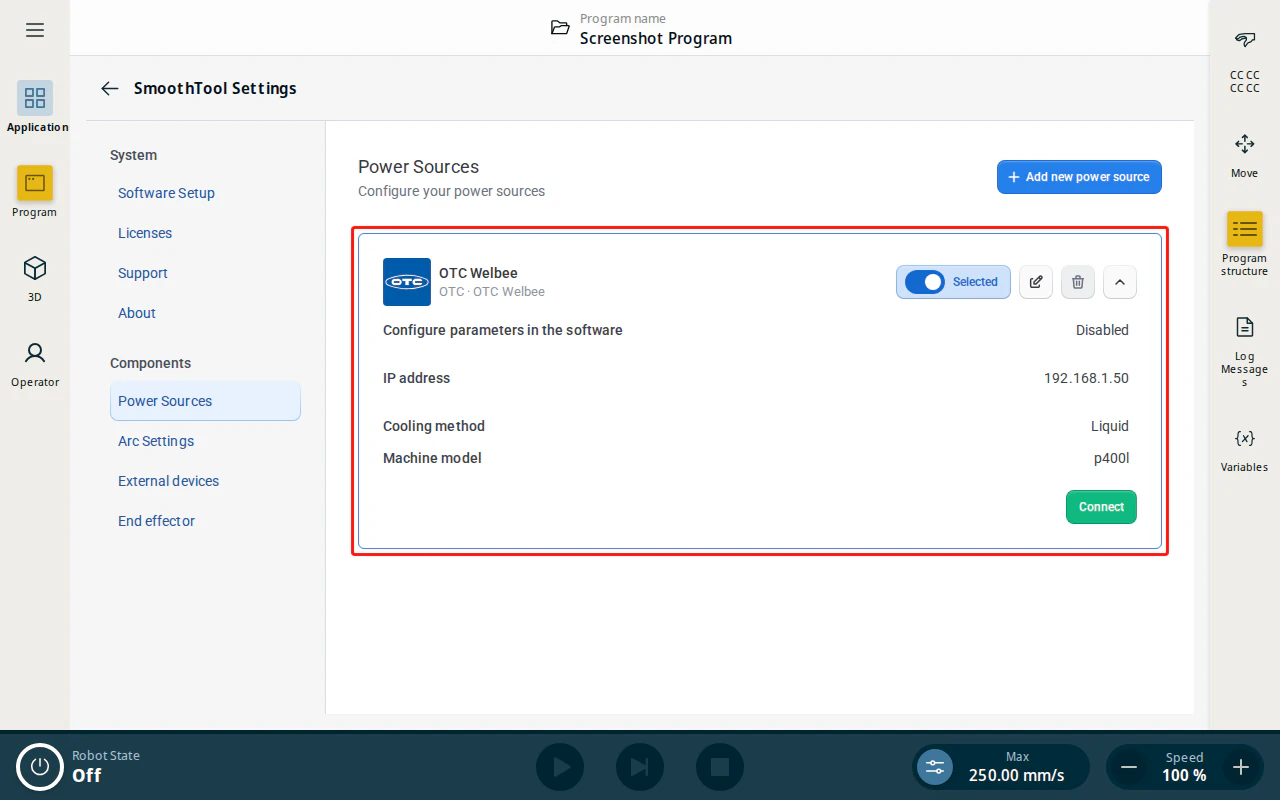
Back on the Power Sources page, expand the new entry, tap Selected to make it the active power source, then tap Connect. When the connection is established, a connection status tag is shown on the entry.
Programming with SmoothTool X and OTC Welbee
When Configure parameters in the software is enabled, you can adjust the welding parameters per node from the program tree.
Select a weld node (e.g. Weld Seam) in the program tree and open its Power source (General) tab. The parameters apply when the program reaches that node.
Process, material, gas and wire selection
The power source uses a synergic line defined by the wire and gas combination. Until one is chosen the node shows a Configure process, material, gas & wire card: tap its edit icon and follow the guided steps to select the Welding method, Wire material, Wire diameter, and Gas.
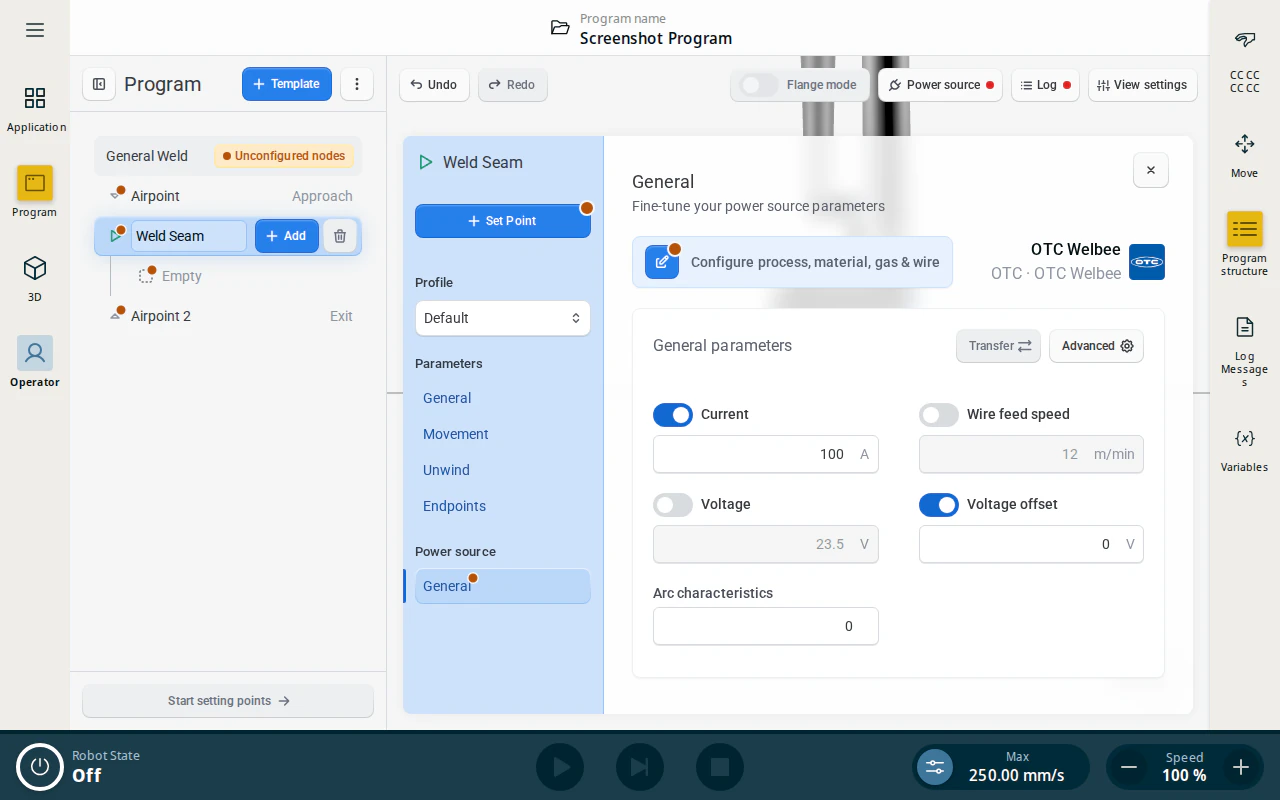
Once the combination is set, the general parameters become available:
| Identifier | Description |
|---|---|
| Process, material, gas & wire | The combination that defines the synergic line, shown as process, material, gas, and wire diameter. Change it with the edit icon. |
| Current / Wire feed speed | Set the welding current directly in amps (A), or toggle to set it by wire feed speed (m/min). |
| Voltage / Voltage offset | Set the welding voltage directly (V), or toggle to a voltage offset from the synergic line. |
| Arc characteristics | Adjusts the arc characteristics. |
| Wave frequency | (DC Wave Pulse welding method only) Adjusts the wave frequency. |
| Transfer | Sends the current parameters to the power source. Available once connected. |
Advanced settings
The Advanced button opens the arc start and end settings, split across a Start and an End tab:
| Identifier | Description |
|---|---|
| Pre-flow / Post-flow time | Gas flow time before the arc starts (Start) and after it ends (End). |
| Initial / Crater current | The current during the initial and crater (end) phases, as a percentage. |
| Initial / Crater time | The duration of the initial and crater phases. |
| Initial / Crater voltage offset | Voltage offset for the initial and crater phases (manual current). |
| Initial / Crater voltage synergy | Voltage fine-tuning for the initial and crater phases (synergic current). |
| Initial / Crater frequency | (DC Wave Pulse only) Wave frequency for the initial and crater phases. |
| Initial / Crater welding method | The welding method used during the initial and crater phases. |
| Turbo start (F13) | Enables or disables Turbo Start. |
Note
The OTC Welbee is the one power source that manages arc timing itself, from its own advanced settings above. SmoothTool X’s Arc Settings therefore do not apply to it: a weld node has no Arc settings tab when an OTC is the active power source, and the device-wide Arc Settings page is not sent to the machine either.
Manual power source controls
The manual controls live in the Power source popover, opened from the button in the operator screen toolbar.
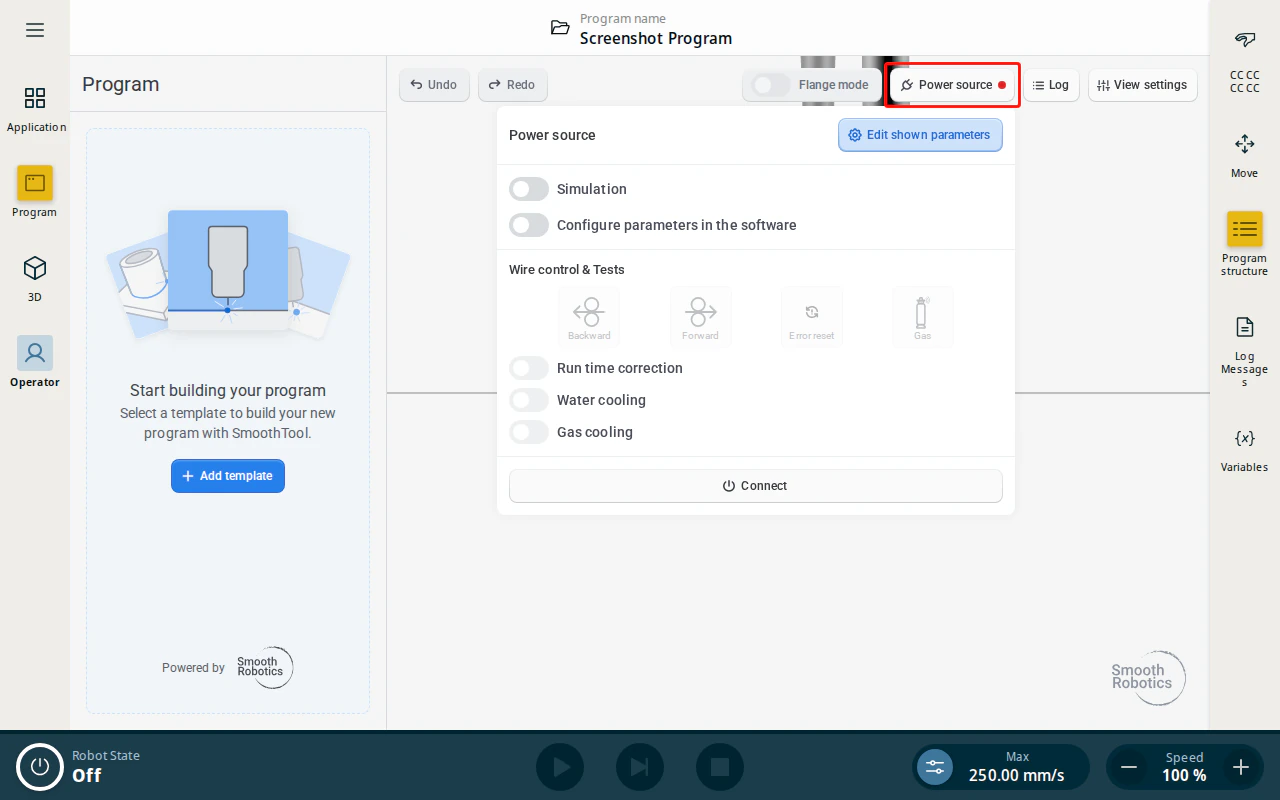
When connected to the OTC Welbee, the following manual controls are available:
| Control | Description |
|---|---|
| Forward | Feeds the welding wire forward. |
| Backward | Retracts the welding wire. |
| Error reset | Sends a reset-error signal to the power source. |
| Gas | Opens the gas valve for the duration of the press. |
| Run time correction | Enables runtime correction of the welding parameters. |
| Water cooling | Toggles the water-cooling function port. |
| Gas cooling | Toggles the gas-cooling function port. |
Warning
Connected to a power source that provides the option to control the wire. Do not use these functions without ensuring no harm can come to people or material. Make sure the area around the welding torch is clear before use.
Simulation
The Simulation toggle at the top of the popover runs the program as a dry run: the robot executes the full program and motion path, but the power source does not weld (no arc, wire feed, or gas). Use it to test a program safely, then turn it off to weld for real.